Plant and capabilities
One shed in Vatva, and two foundries down the road
We machine, assemble, test, mark and pack in our own works. Castings come from foundries in the same estate, poured to our patterns and checked by us before we accept them.
- covered shed, Vatva GIDC Phase II
- 2,400 m²
- people, on one shift (two in season)
- 46
- bronze valves a month, 15 to 50 mm
- ≈ 9,000
- cast-steel valves a month, 50 to 300 mm
- ≈ 350
The route card
Every batch travels the works with a route card. These are its operations, in order, and the check before each one signs off.
Operation 10: Castings in
Bronze castings are poured for us by two foundries in Vatva GIDC; stainless investment castings come from Rajkot. Each lot arrives with the foundry's chemical report.
Two foundries in Vatva GIDC; one in Rajkot
Check: Chemistry checked against IS 318 or ASTM by an outside lab, one sample per heat; visual check of every casting.
Operation 20: Machining
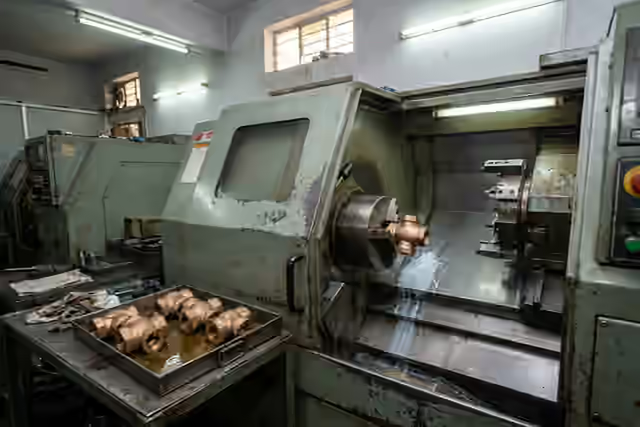
Bodies, bonnets and wedges are faced, bored and threaded on CNC turning centres; flanges drilled on a radial drill.
In-house
Check: Threads gauged with ring and plug gauges, every 10th piece and the first of every setup.
Operation 30: Assembly
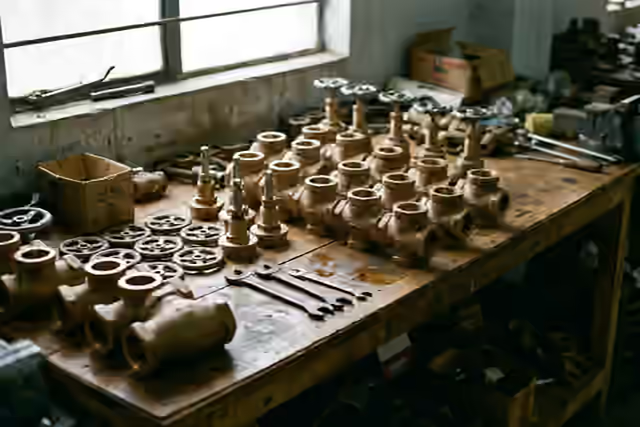
Stems, wedges and discs are fitted, seats lapped, glands packed and handwheels fitted on two assembly lines.
In-house
Check: Seat contact checked with engineer's blue on every wedge and disc.
Operation 40: Pressure test
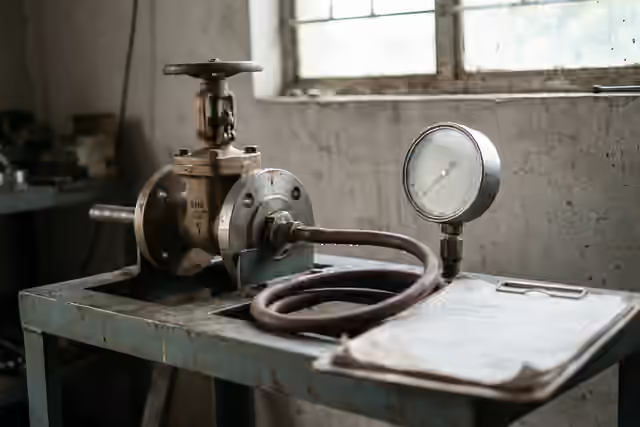
Every valve is shell- and seat-tested with water on the test bench, at the pressures its standard sets.
In-house
Check: Pass or fail recorded against the batch or heat number; a fail goes back to assembly.
Operation 50: Marking and finish
The batch number is stamped beside the cast marks; cast-steel valves are painted and tagged.
In-house
Check: Markings checked against the order and MSS SP-25.
Operation 60: Packing
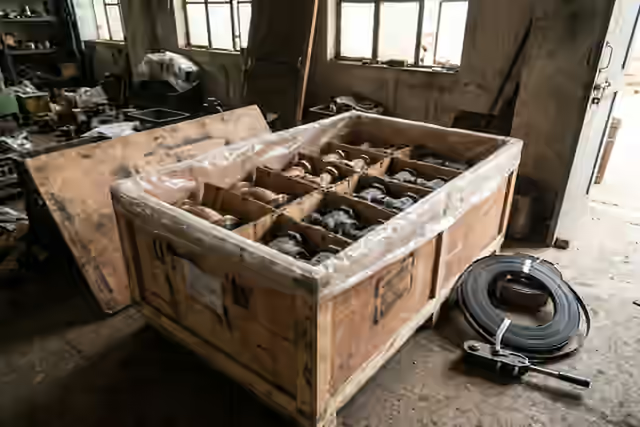
Valves are capped, bagged and packed in cartons, or in heat-treated plywood cases for export.
In-house
Check: Packing list checked against the order, piece by piece.
Machines
| Machine | How many | Capacity | Used for |
|---|---|---|---|
| CNC turning centre | 4 | Up to 250 mm turning diameter | Bronze bodies, bonnets and wedges, 15 to 80 mm |
| CNC turning centre, large | 1 | Up to 500 mm turning diameter | Cast-steel bodies and bonnets, 50 to 300 mm |
| Vertical machining centre | 1 | 800 × 500 × 500 mm | Bonnet faces, actuator pads |
| Radial drilling machine | 2 | Up to 50 mm drill | Flange drilling |
| Capstan lathe | 6 | Up to 40 mm bar | Stems and small parts |
| Hydrostatic test bench | 3 | Up to 15 MPa | Shell, seat and backseat tests |
| Air test bench | 1 | Up to 0.7 MPa | Air seat tests on request |
Tests
| Test | How | To | Which pieces |
|---|---|---|---|
| Shell test, hydrostatic | At 1.5 × rated pressure, held 60 s or longer, no visible leak or sweating | IS 778 · API 598 | Every valve |
| Seat test, hydrostatic | At 1.1 × rated pressure on each side of the closed valve | IS 778 · API 598 | Every valve |
| Backseat test | Stem backseated, gland loose, shell pressure | API 598 | Every cast-steel gate valve |
| Chemical analysis | Spectrometer analysis of a sample from each heat, by an outside NABL lab | IS 318 · ASTM A216 · A351 | One per heat |
| Dimensional check | Face to face, threads and flange drilling against the drawing | ASME B16.10 · IS 554 | First piece and 1 in 10 |
Capacity, honestly
We are a small works. For an urgent order of more than 2,000 bronze valves, or more than 50 cast-steel valves, ask before you promise your customer a date: we'll tell you honestly.
What we don't do in-house
- Foundry work: we don't pour metal; our castings come from three foundries we have used for over ten years.
- Radiography and other NDT: arranged through an outside agency when an order asks for it.
- Actuators: we supply the ISO 5211 pad; actuators are bought in on request.
Send us the drawing. We'll send a price.
A quote with price, lead time, test pressures and packing, within two working days.
Within 2 working hours
A reply from a person, with a request number, asking anything we need to know.
Within 2 working days
The quote, as a PDF by email. Drawings to order may take a day longer.
When you order
A proforma invoice and the delivery date we'll keep. Bronze stock sizes ship within a week.